Some Known Details About R Vand Technology
Table of ContentsGetting The R Vand Technology To WorkR Vand Technology Can Be Fun For AnyoneThe Facts About R Vand Technology UncoveredThe Single Strategy To Use For R Vand TechnologyR Vand Technology Can Be Fun For Anyone
, various other makers and tools are also set up with the equivalent CNC, which makes the production industry in its support, considerably enhancing the high quality and performance. (3D printing) to create a brand-new production technique - crossbreed additive subtractive production (HASM).CNC machine Summary Image Equates programs consisting of specific numbers and letters to relocate the pin (or workpiece) to different locations and depths. Can either be an Upright Milling Facility (VMC) or a Straight Milling Facility, depending on the positioning of the spindle.
Many CNC mills need placing the workpiece on or in them and have to go to least as large as the work surface, however new 3-axis machines are being produced that are much smaller sized. Cuts workpieces while they are rotated. Makes quick, accuracy cuts, normally utilizing indexable tools and drills. Efficient for difficult programs designed to make parts that would certainly be impossible to make on manual turrets.
The Facts About R Vand Technology Revealed

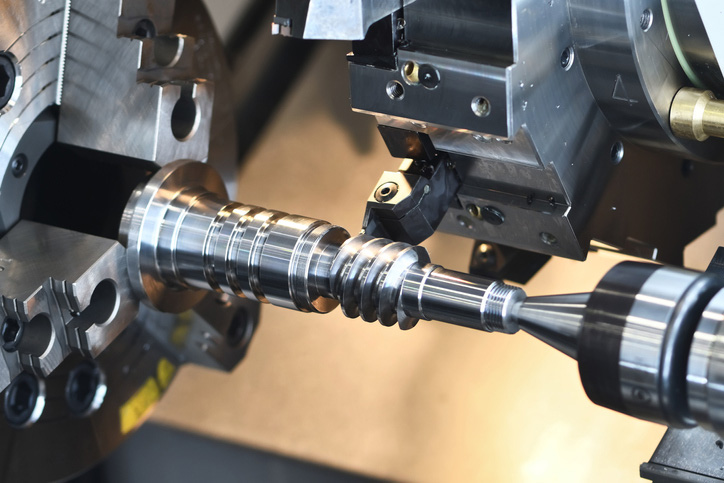
Typically have 2 axes (X and Z), yet more recent models have more axes, enabling for even more advanced tasks to be machined. A lot of modern-day turrets have real-time tooling, enabling minimal milling operations to happen without needing to get rid of the component from the turret pin. Second operations can be finished by using a sub-spindle, which is co-axial to the primary pin, yet deals with the other direction.
Typically used to reduce steel and other steels, yet can be utilized on a range of materials.
EDM can be broadly separated into "weight" type procedures, where the electrode is the favorable shape of the resulting attribute in the component, and the electrical discharge erodes this attribute into the part, resulting in the unfavorable shape, and "cord" type procedures. Sinker processes are instead sluggish as compared to standard machining, balancing like 100 mm3/min, as contrasted to 8 million mm3/min for traditional machining, yet it can generate features that traditional machining can not.
R Vand Technology Can Be Fun For Anyone
This is useful for complicated accounts with within 90 degree corners that would certainly be challenging to maker with standard methods. Electrolyte solution saturates the workpiece, and voltage is used in between the sinker, top, and workpiece, base. Considered to be extremely efficient by enhancing performance with automation.
Multi-spindle devices have multiple pins on a drum that rotates on a straight or upright axis. There are two types of attachments for these drill heads, dealt with or adjustable, depending on whether the center range of the boring pin needs to be differed (cnc milling service).
R Vand Technology for Dummies
Some waterjet cutters have a 5-axis cutting head, permitting far more complicated shapes to be cut, and to make up for the angle of the kerf to leave the angled wall surface on the supply rather than on the completed component. Waterjet reducing device Made use of to quickly punch openings and cut thin products.
Punch presses are generally used when a CNC mill would certainly mishandle or impractical. https://blackgreendirectory.com/gosearch.php?q=https%3A%2F%2Fwww.r-vandtech.com%2F&search-btn.x=36&search-btn.y=35. CNC punch presses can can be found in the C structure, where the sheet product is secured onto a machining table and a hydraulic ram lowers on the product, or they can can be found in a portal frame variation where bar stock/tubing is fed right into the machine
A mild accident may not harm the equipment or devices but may damage the component being machined to ensure that it must be junked. Several CNC tools have no integral sense of the absolute position of the table or tools when transformed on. They need to be manually "homed" or "zeroed" to have any referral to work from, and these limits are simply for determining the location of the component to function with it and are no hard activity limit on the device.
How R Vand Technology can Save You Time, Stress, and Money.
Machines equipped with lots sensors can quit axis or spindle activity in reaction to an overload problem, however this does not prevent an accident from taking place. It may just limit the damage resulting from the collision. Some collisions may never overload any kind of axis or pin drives. If the drive system is weak than the maker's architectural honesty, then the drive system just presses against the obstruction, and the drive electric motors "slip in place".